Splay Marks in Injection Molding: Causes, Fixes, and Prevention
Splay Marks in Injection Molding: Causes, Fixes, and Prevention

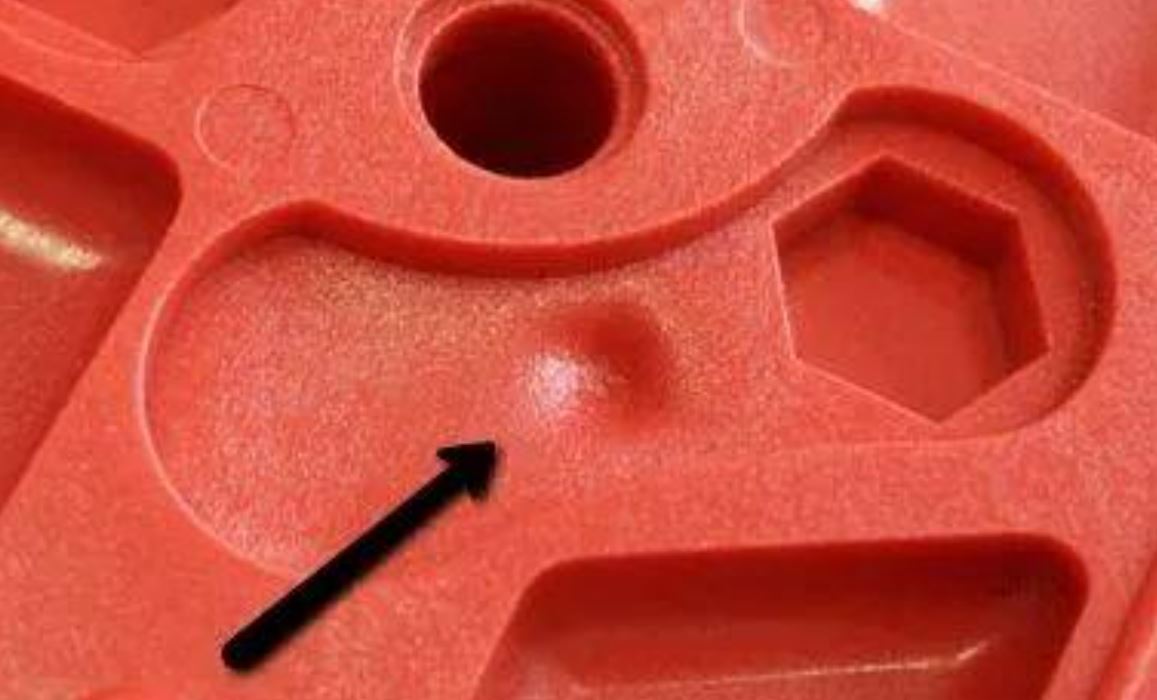
If you have ever seen silvery-white streaks on a black or dark injection molded part, you have seen splay marks. In the industry, they are also called silver streaks, moisture marks, or jetting lines. They look like small scratch marks radiating from the gate area across the surface of the part.
Splay marks are one of the most common surface defects in injection molding. They do not usually affect the strength of the part, but they make the part look bad and can cause quality rejection — especially for visible parts like housing, covers, and consumer products.
This guide explains what causes splay marks, how to tell them apart from other defects, and how to fix and prevent them. Based on years of injection molding experience at Eastmaster Manufacturing Limited in Shenzhen.
What Are Splay Marks?(H2)
Splay marks are silvery-white streak patterns on the surface of an injection molded part. They typically appear near the gate (where the plastic enters the mold) and spread outward in a fan-like pattern.
Key features of splay marks:
Silvery or white streak lines on the part surface
Usually near the gate area, spreading outward
More visible on dark-colored parts (black, dark blue, dark green)
Surface-level defect — does not go deep into the part
Can appear on any thermoplastic material (ABS, PC, Nylon, POM, PP, etc.)
Splay marks are different from flow lines (which follow the melt flow direction) and weld lines (which appear where two melt fronts meet). The silvery color comes from tiny gas bubbles or moisture that get stretched into thin lines during filling.
Root Causes of Splay Marks(H2)
Splay marks have several root causes. The most common ones are listed below, from most frequent to least.
1. Insufficient Material Drying(H3)
This is the #1 cause of splay marks, especially for materials that absorb moisture from the air (called hygroscopic materials). Nylon (PA), PC, ABS, and PET all absorb moisture easily.
When wet plastic pellets go into the injection machine, the water inside turns to steam at high melt temperatures (200-300°C). The steam creates tiny gas bubbles in the melt. As the melt fills the mold, these bubbles get stretched into long thin lines — that is the splay mark you see.
Typical drying requirements:
ABS: 80-85°C for 2-4 hours, moisture content below 0.05%
PC: 120°C for 3-4 hours, moisture content below 0.02%
Nylon (PA6, PA66): 80-90°C for 4-6 hours, moisture content below 0.1%
PET: 150-160°C for 4-6 hours, moisture content below 0.005%
PP, PE: Usually do not need drying (non-hygroscopic), but 60-80°C for 1 hour if stored in humid conditions
2. Mold Temperature Too Low(H3)
When the mold surface is too cold, the melt cools down too fast as soon as it touches the mold wall. The surface layer freezes before it can smooth out, trapping gas marks and flow marks in the surface. This is especially common in cold weather or when the mold temperature controller is not set correctly.
Typical mold temperature ranges:
ABS: 50-80°C
PC: 80-120°C
Nylon: 60-100°C
POM: 80-120°C
Rule of thumb: higher mold temperature gives better surface finish but longer cycle time. Find the balance for your part.
3. Poor Gate Design(H3)
The gate is where the plastic enters the mold cavity. If the gate is too small, in the wrong position, or the wrong type, it can cause the melt to shoot into the cavity like a jet (called jetting) instead of flowing smoothly. This jetting creates fold lines and splay marks on the surface.
Common gate design problems:
Gate too small: High injection speed through a small opening causes jetting
Gate position wrong: Gate pointing directly at a large open area causes the melt to shoot across instead of filling from the gate outward
Wrong gate type: Using a pinpoint gate for a large part, or a fan gate for a small thin part
Fix: use a properly sized gate, place it so the melt hits a wall or core first (not open space), and choose the right gate type for the part size and shape.
4. Injection Speed Too Fast(H3)
When the injection speed is too high, the melt enters the mold cavity too fast and creates a jetting effect. The melt shoots across the cavity instead of filling it layer by layer. This causes surface marks, trapped air, and splay.
Fix: slow down the injection speed, especially in the first stage of filling. Use a multi-stage injection profile — slow at the start, faster in the middle, slow again at the end.
5. Melt Temperature Too High(H3)
When the barrel temperature is set too high, the plastic can start to break down (degrade). Degraded plastic releases gas, which creates splay marks. This is more common with heat-sensitive materials like PVC and POM.
Fix: check the material data sheet for the recommended melt temperature range, and stay within it. If you need higher flow, try increasing mold temperature instead of melt temperature.
6. Insufficient Back Pressure(H3)
Back pressure is the pressure applied to the screw during the plasticizing (melting) stage. Low back pressure means the screw turns fast and does not push the melt hard enough. This leaves air bubbles and unmelted pockets in the melt, which show up as splay marks on the part.
Fix: increase back pressure to 5-15 bar (depending on material). This compresses the melt, pushes out air, and gives a more uniform melt.
How to Tell Splay Marks Apart from Other Defects(H2)
|
Defect |
Appearance |
Location |
Main Cause |
|
Splay Marks (Silver Streaks) |
Silvery-white thin lines, fan-shaped |
Near gate, spreading outward |
Moisture, low mold temp, jetting |
|
Flow Lines |
Wavy lines following melt flow direction |
Along flow path, near gate |
Low melt temp, slow injection |
|
Weld Lines |
Visible line where two melt fronts meet |
Around holes, behind bosses |
Melt fronts meeting at low temp |
|
Burn Marks |
Brown or black discoloration |
End of fill, air traps, thin areas |
Trapped air compressed and heated |
|
Short Shot |
Incomplete part, missing sections |
Far end of flow path |
Not enough material, low pressure |
Quick tip: if you can scrape the silvery mark with your fingernail and it feels slightly rough, it is likely splay. If it looks like a smooth wavy line, it is more likely a flow line.
Step-by-Step Fix Guide(H2)
When you see splay marks on a part, follow this order to find and fix the root cause:
Step 1 — Check material drying: Is the dryer working? Is the drying temperature correct? Is the drying time long enough? Test the moisture content with a moisture analyzer. This fixes 70% of splay problems.
Step 2 — Check mold temperature: Use a surface thermometer to verify the actual mold temperature. Is it within the recommended range for the material? If too low, increase it gradually (5-10°C at a time).
Step 3 — Check injection speed: Slow down the first stage injection speed by 20-30%. If splay improves, you found the cause. Then fine-tune to find the best speed.
Step 4 — Check melt temperature: Verify the actual melt temperature with a purge test. If too high, reduce by 10-20°C. If too low, increase slightly.
Step 5 — Check back pressure: Increase back pressure by 3-5 bar and see if splay improves.
Step 6 — Check gate design: If all the above fail, the problem may be in the mold design. Review gate size, position, and type. This may need mold modification.
Prevention Tips for Long-Term Quality(H2)
Always dry hygroscopic materials: Set up a standard drying procedure for each material and follow it every time. Do not skip drying to save time.
Use a moisture analyzer: Check the moisture content of dried pellets before production. This takes 5 minutes and prevents hours of bad parts.
Control workshop humidity: In humid seasons (rainy season in South China, summer in many regions), dried pellets can re-absorb moisture within 30 minutes of leaving the dryer. Use closed-loop drying systems or keep pellets in sealed containers.
Maintain mold temperature controllers: Check water lines, pumps, and heaters regularly. A broken mold temp controller is a common hidden cause of sudden splay.
Record process parameters: Save the good settings for each part and material. When splay appears again, compare with the saved settings to find what changed.
Train operators: Many splay problems come from operators skipping drying steps or changing settings without understanding why. Train your team on the "why" not just the "how."
Why Choose Eastmaster for Injection Molding(H2)
At Eastmaster Manufacturing Limited, quality control starts before the first shot. We check every batch of material for moisture content, verify mold temperatures before production, and monitor process parameters throughout the run.
In-house material drying with dehumidifying dryers for all hygroscopic materials
Moisture content testing before every production run
• >Precise mold temperature control on all injection machines
• >First article inspection with detailed surface quality checks
Process parameter documentation for repeatable quality
ISO 9001 and ISO 13485 certified quality management
D-U-N-S verified: 66-849-8033
Whether you need help troubleshooting splay marks on an existing part, or want to start a new injection molding project with the right process from the start, our engineering team is here to help. Contact Eastmaster today with your part details for a free process review.

• Email: info@eastmaster.com
• Phone: +86 755 22676100
• WhatsApp / WeChat available on the right side.
CNC Machining Tolerances: What's Achievable and How to Spec Them